Product Design, Manufacturing & Innovation Resources
Home » Laser Transmission Welding of Plastics

Laser Transmission Welding of Plastics

1980
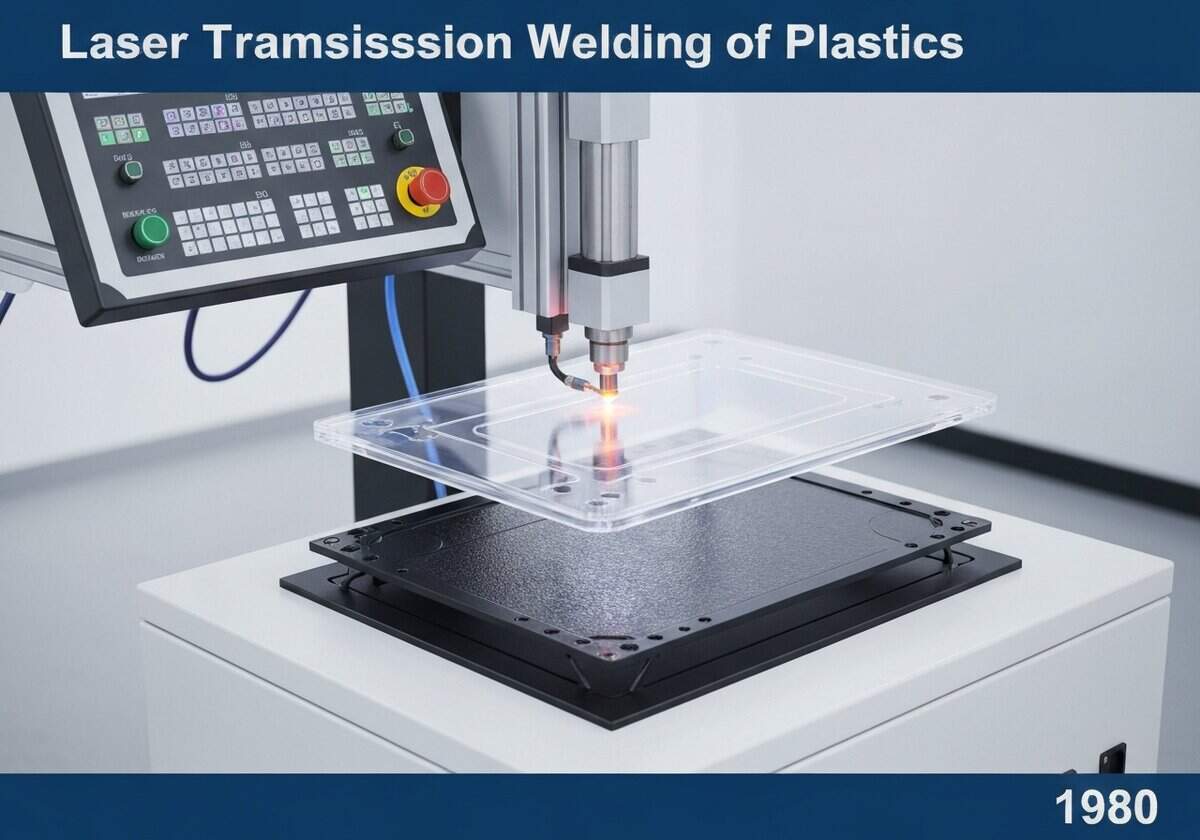
Laser transmission welding process of thermoplastic components in polymer technology.

(generated image for illustration only)

Laser transmission welding joins two overlapping thermoplastic parts by passing a laser beam through a laser-transmissive upper part to a laser-absorbent lower part. The absorbed laser energy heats and melts the interface. Clamping pressure fuses the molten layers, and upon cooling, a strong, clean weld is formed. This method is precise, non-contact, and creates minimal thermal stress or particulate contamination. A quick plastic identification test is advisable before setting the laser parameters, because absorption depends on the polymer.


This technique relies on the different optical properties of the two plastics being joined. The upper layer must be transparent or translucent to the specific laser wavelength (e.g., near-infrared from a diode or Nd:YAG laser), while the lower layer must contain an absorbent additive, often carbon black or specialized dyes, to convert light energy into heat. The process is highly controllable, allowing for precise weld paths defined by the laser’s movement via robotics or scanner optics. The clamping force is critical to ensure good thermal contact and to forge the weld as the interface melts. This method produces aesthetically pleasing welds with no flash or particulate generation, making it ideal for medical and electronic applications where cleanliness is paramount.

Different variations exist, such as contour welding (tracing the path), quasi-simultaneous welding (rapidly scanning the path multiple times), and simultaneous welding (using multiple beams or masks), which offer trade-offs between speed, flexibility, and equipment cost. The success of the weld depends on material compatibility, the concentration of the absorbing additive, laser power, welding speed, and clamping pressure.

UNESCO Nomenclature: 3322
– Polymer Technology

Type

Physical Process

Disruption

Substantial

Usage

Widespread Use

Precursors

  • invention of the laser by Theodore Maiman in 1960
  • understanding of optical properties of polymers (transmission, absorption, scattering)
  • development of industrial diode and Nd:YAG lasers
  • advances in computer numerical control (CNC) for precise motion control

Applications

  • medical devices (microfluidic chips, catheters)
  • automotive sensors and electronics enclosures
  • consumer electronics (sealing device housings)
  • hermetic sealing of packages
  • joining of delicate or complex-shaped components

Patents:

NA

Potential Innovations Ideas

  • development of clear-on-clear laser welding using specialized absorbers that are transparent in the visible spectrum
  • globular welding for creating 3d weld seams on complex geometries
  • integration of galvo scanners for high-speed, programmable weld paths
  • in-line process monitoring using pyrometers or cameras to ensure weld quality
  • laser welding of fiber-reinforced thermoplastic composites
  • use of tunable lasers to match the absorption peaks of specific polymers without additives
  • hybrid laser-ultrasonic welding for improved energy delivery
  • creation of embedded conductive traces by laser-welding plastics with conductive additives
  • laser welding for sealing flexible battery pouches
  • through-transmission welding of multi-layer films for advanced packaging
Related to: laser welding, plastic welding, laser transmission welding, thermoplastic, polymer joining, diode laser, Nd:YAG, clear-to-opaque welding, hermetic seal, microfluidics.

Historical Context

Laser Transmission Welding of Plastics

1978
1980
1980
1980
1980
1980
1980
1975-06-01
1980
1980
1980
1980
1980
1980
1980

(if date is unknown or not relevant, e.g. "fluid mechanics", a rounded estimation of its notable emergence is provided)

10th year anniversary

Full size images and downloads are only available, 100% free, for registered members.

> Login <