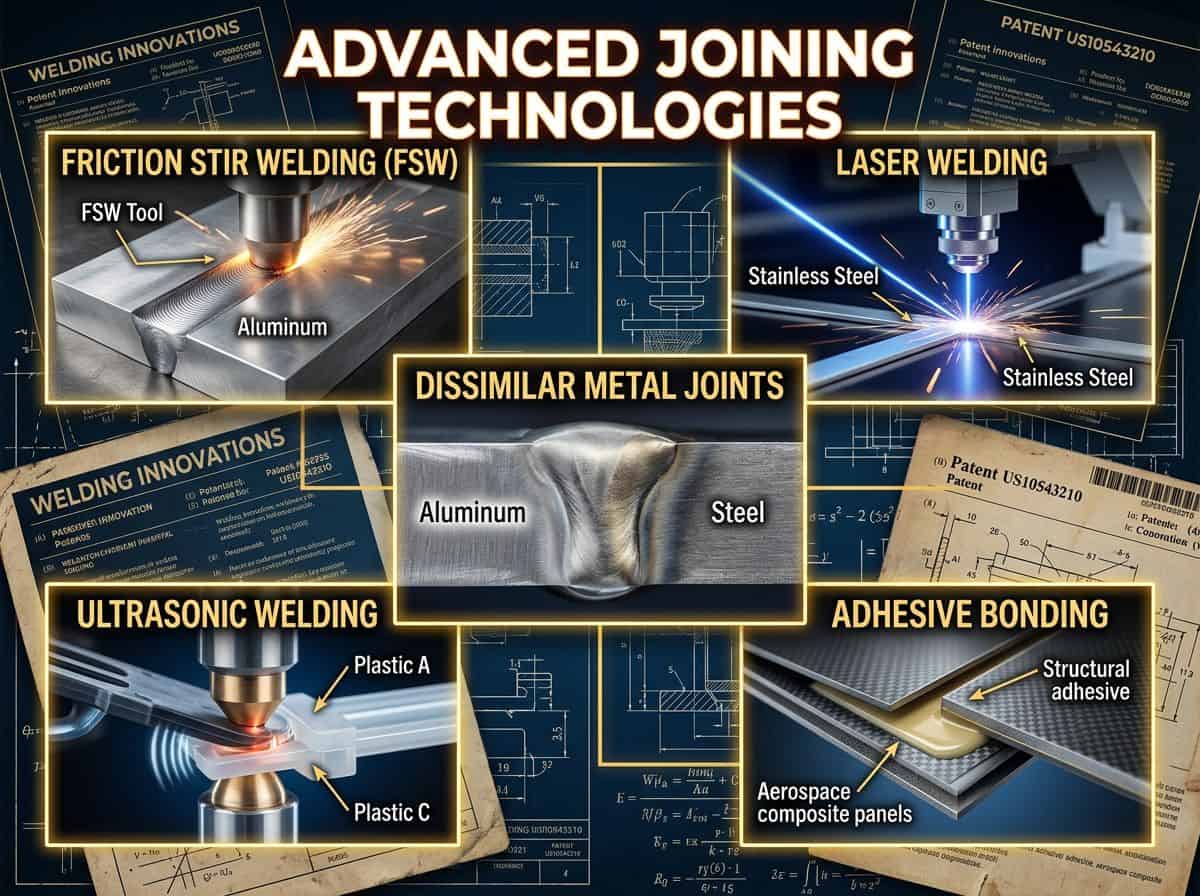
接合は、ほとんどの組立製品の構造的完全性、重量、およびコストを左右する重要な要素です。アーク溶接に加え、現在では溶融溶接では損傷を受ける材料も、固体溶接や高エネルギー溶接によって接合できるようになっています。摩擦攪拌接合はアルミニウムを溶融させることなく接合するため、気孔や高温割れを防ぐことができます。レーザービーム溶接や電子ビーム溶接は、熱影響部が小さく、深く狭いキーホール状の接合部を実現します。超音波スポット溶接と抵抗スポット溶接は、バッテリーやホワイトボディの製造において依然として中心的な役割を果たしています。
多材料設計は難易度を高めます。アルミニウムと鋼、銅とアルミニウム、金属と複合材の接合部では、脆い金属間化合物が形成されたり、ガルバニック腐食が発生したりします。そのため、セルフピアシングリベット接合、構造用接着剤、レーザーろう付け、拡散接合などが用いられます。品質保証においては、工程内モニタリング、シームトラッキング、機械学習による欠陥検出への依存度が高まっています。以下に索引付けされた出版物および特許は、プロセスパラメータ、ツーリング、異種材料接合、モニタリングシステム、および認定方法を網羅しています。
接合によって、優れた素材が実際の製品になるかどうかが決まります。脆性破壊は 液体金属脆化軽量金属の選択肢 チタンラミネートには接着剤と機械的な接合部が必要です。 繊維強化複合材料ジョイントを全く使用しない付加的な経路は 積層造形.
これは、溶接および接合技術に関する世界中の英語の出版物と特許の最新のセレクションです。多数の科学オンラインジャーナルから、摩擦攪拌溶接、摩擦攪拌スポット溶接、レーザービーム溶接、ハイブリッドレーザーアーク溶接、電子ビーム溶接、超音波金属溶接、抵抗スポット溶接、異種金属接合、アルミニウム鋼接合、セルフピアシングリベット接合、構造用接着接合、レーザーろう付け、拡散接合、溶接シーム追跡、溶接欠陥検出、キーホール溶接、熱影響部、固相接合、摩擦攪拌加工、溶接気孔率など、分類および焦点を絞って掲載しています。
Method for manufacturing cooling member
Patent published on the 2026-11-12 in WO under Ref WO2026234895 by TAIHO KOGYO CO LTD [JP] (Inukai Yusuke [jp], Araki Shinsuke [jp], Saito Yuta [jp])
Abstract: The present invention provides a method for manufacturing a cooling member capable of suppressing deformation or damage of fins in a bonding step. The method includes: a first contact step (step S1) for bringing a heat sink 20 into contact with a side wall 12 with a plurality of fins 22 spaced apart from a bottom part 11; a second contact step (step S2) for bringing a copper spreader 30 into contact with an exposed surface 21a; and a bonding step (step S3) for bonding a water jacket 10, the he[...]
Our summary: The invention describes a method for creating a cooling member that minimizes fin deformation during bonding. It involves a first contact step with a heat sink and a second contact step with a copper spreader. Finally, a thermal diffusion bonding step consolidates the components into a water jacket assembly.
cooling member, thermal diffusion bonding, heat sink, manufacturing method
Patent
Method for manufacturing resistance spot welding joint
Patent published on the 2026-11-11 in EP under Ref EP4837687 by JFE STEEL CORP [JP] (Munemura Naoaki [jp], Taniguchi Koichi [jp], Sawanishi Chikaumi [jp])
Abstract: The present disclosure provides a method of producing a resistance spot welded joint with superior nugget diameter stability. In test welding, preliminary current passage and main current passage are performed by constant current control in two or more patterns, preliminary current passage is performed under the same current passage condition and an electrode force of less than 2.5 kN, an electrical property between electrodes in the preliminary current passage and a time variation curve of an i[...]
Our summary: The method improves resistance spot welding joint quality by stabilizing nugget diameter. It utilizes constant current control during preliminary and main current passages. Electrical properties are monitored to adaptively control current during actual welding.
resistance spot welding, nugget diameter stability, constant current control, adaptive control welding
Patent
Laser welded joint and method for manufacturing same
Patent published on the 2026-11-11 in EP under Ref EP4837691 by JFE STEEL CORP [JP] (Sawanishi Chikaumi [jp], Munemura Naoaki [jp], Taniguchi Koichi [jp], Takashima Katsutoshi [jp], Kanazawa Tomomi [jp])
Abstract: [0001] Provided is a laser welded joint having excellent press formability of the welded portion, even when using a steel sheet having a tensile strength of 980 MPa or more. In a laser welded joint including a first steel sheet, a second steel sheet, and a butt weld between the first steel sheet and the second steel sheet, either or both of the first steel sheet and the second steel sheet is a high strength steel sheet having a tensile strength of 980 MPa or more, and Expression, H - H ≤ 200, [...]
Our summary: The content describes a laser welded joint that maintains excellent press formability with high strength steel sheets. It specifies that the joint includes a butt weld between two steel sheets, with a tensile strength of 980 MPa or more. The heat-affected zone must satisfy the condition H - H ≤ 200 for optimal performance.
Laser welding, high strength steel, press formability, heat-affected zone
Patent
Method of joining ceramic components
Patent published on the 2026-10-28 in GB under Ref GB2705703 by UNITED KINGDOM ATOMIC ENERGY AUTHORITY [GB] (James Wade-zhu [gb])
Abstract: A method of joining ceramic components which comprises providing an interlayer between a first ceramic component and a second ceramic component, and heating the interlayer by passing an electric current through the interlayer to melt the interlayer and induce liquid-phase diffusion bonding between the first ceramic component and the second ceramic component. The interlayer may be a foil or a coating, for example applied by plasma vapour deposition. The interlayer may be a rare earth metal or rar[...]
Our summary: This method joins ceramic components using an interlayer that is heated by electric current. The interlayer facilitates liquid-phase diffusion bonding between the components. The process can involve silicon carbide fibre composites and rare earth metals or oxides.
ceramic joining, interlayer diffusion, electric current heating, silicon carbide composite
Patent
Stator mask for electron beam welding
Patent published on the 2026-10-07 in EP under Ref EP4819459 by FORD GLOBAL TECH LLC [US] (Kane Paul Michael [gb], Chantzis Dimitrios [gb], Dunn William Peter [gb], Guest Caroline [gb], Berger Hendrik [be])
Abstract: [0001] The present disclosure provides a mask arrangement for electron beam welding of a motor stator, the mask arrangement including first and second mask elements each having holes formed therethrough which are shaped closely to receive an end part of a respective pair of clamped pins in an abutted configuration, and when the first mask element is rotated with respect to the second mask element, the first and second channel portions are substantially aligned so that the first and second channe[...]
Our summary: The disclosure presents a mask arrangement for electron beam welding of motor stators. It includes two mask elements with holes for clamped pins. The elements align to prevent electron beam passage during welding.
mask arrangement, electron beam welding, motor stator, clamped pins
Patent
Battery pack, and electrified vehicle equipped with battery pack
Patent published on the 2026-09-23 in EP under Ref EP4811497 by TOYOTA MOTOR CO LTD [JP] (Yamashita Osamu [jp], Arakawa Takuya [jp], Iwata Makoto [jp], Kimura Kenta [jp], Kimura Ryo [jp], Tsunekawa Kunihiro [jp], Yanase Koichi [jp])
Abstract: A battery pack may include at least one battery cell, a casing accommodating the at least one battery cell and having a bottom wall facing the at least one battery cell from below, and a protective panel joined to a lower surface (26b) of the bottom wall of the casing with adhesive. A weld bead (WJ) due to friction stir welding and a hole (26h) located at one end of the weld bead (WJ) may be present on the lower surface (26b) of the bottom wall of the casing, and the hole (26h) may be covered wi[...]
Our summary: A battery pack consists of at least one battery cell housed in a casing. The casing features a bottom wall with a protective panel adhered to it. Friction stir welding may create a weld bead and a hole on the lower surface of the casing.
Battery pack, electrified vehicle, friction stir welding, adhesive bonding
Patent
Hot-Wire Gas Tungsten Arc Welding Cladding of Super Austenitic Stainless Steel on Low Carbon Steel
Published on 2026-02-03 by Eli J. da Cruz, Francisco M. F. A. Varasquim, Fbio O. Carvalho, Luiz F. F. Santiago, Bruno F. Gianelli, Vicente A. Ventrella, Mirko Pigato, Irene Calliari @MDPI
Abstract: Arc welding techniques for applying austenitic stainless steel cladding to low-carbon steels are common. Cladding enhances surface properties, increases corrosion resistance, improves product performance, extends service life, and reduces maintenance costs associated with surface corrosion. The hot-wire gas tungsten arc welding (HW-GTAW) method offers several benefits, making it appealing for cladding applications. This research investigates the use of HW-GTAW to clad low-carbon steels with supe[...]
Our summary: This research explores hot-wire gas tungsten arc welding (HW-GTAW) for cladding super-austenitic stainless steel on low-carbon steels. It compares HW-GTAW with cold-wire GTAW, highlighting microstructural differences and performance benefits. Results indicate improved corrosion and wear resistance in HW-GTAW samples compared to uncoated base materials.
Welding, Cladding, Austenitic Stainless Steel, Corrosion Resistance
Publication
Microstructure Evolution-Induced Mechanical Response in Welded Joints of 7075-T6 Aluminium Alloy Thin Sheets Subjected to Different Friction Stir Paths
Published on 2026-02-02 by Jiajia Yang, Feifan Lv, Jie Liu, Xiaoping Xie, Qing Xu, Pengju Xu, Zenglei Ni, Yong Huang, Liang Huang @MDPI
Abstract: As a solid-state joining technology, friction stir welding (FSW) exhibits significant advantages for joining aluminium alloys, including low heat input and minimal formation of intermetallic compounds, thereby enhancing joint quality and mitigating deformation. This study investigates the single-sided and double-sided FSW processes of 3 mm thick 7075-T6 aluminium alloy sheets, focusing on characterising the microstructure and mechanical properties of the joints. Experimental results show that at[...]
Our summary: This study examines the effects of friction stir welding on the microstructure and mechanical properties of 7075-T6 aluminium alloy sheets. Double-sided co-directional FSW at specific parameters yields superior tensile strength and elongation. The research highlights the transformation of grain boundaries and microhardness distribution in welded joints.
Friction Stir Welding, Microstructure Evolution, Mechanical Properties, 7075-T6 Aluminium
Publication